Welcome to Our Factory for a Visit! Free customized disinfection solutions
In the world of chocolate and confectionery, pure flavor and stable crystal structure are essential to product quality. Tempering equipment plays a critical role in achieving these characteristics, making proper cleaning and disinfection particularly important. Chlorine dioxide, with its broad-spectrum disinfection capability, is commonly used in food-processing facilities. However, after disinfection, controlling chemical residues on equipment surfaces to an acceptable level—while avoiding unnecessary impacts on flavor, surface quality, or process stability—requires careful management.
Chocolate tempering is a highly precise process. If abnormal chemical residues, moisture, or odors remain after cleaning and disinfection, they may affect subsequent production conditions and create risks to product flavor, surface appearance, and process stability.
In confectionery production, abnormal chemical residues may also introduce off-odors, affect surface quality, or interfere with downstream processing stability.
Therefore, residue control after disinfection is important not only for hygiene management, but also for product quality and production consistency.
Chlorine dioxide disinfectants intended for the relevant food-processing application should be used, and preparation and application should strictly follow the product instructions.
The working concentration should be determined according to the specific product instructions, target microorganisms, equipment-surface conditions, and the company’s validated procedures. A concentration of 50–100 mg/L should not be treated as a universal recommendation for all chocolate-processing equipment surfaces.
While maintaining validated disinfection performance, unnecessarily high concentrations and overdosing should be avoided. Calibrated or validated measuring equipment should be used, and working solutions should be prepared as required for immediate use.
Pretreatment: Before disinfection, grease, sugar deposits, and other organic residues should be removed according to the hygienic design of the equipment and the company’s cleaning procedures. Such organic matter may increase chlorine dioxide demand, reduce the effective concentration available for disinfection, and interfere with adequate contact between the disinfectant and target microorganisms.
It is especially important to recognize that chocolate is a low-moisture food and is highly sensitive to water. Whether equipment is suitable for wet cleaning, spraying, or rinsing should first be determined according to equipment hygienic design and the company’s cleaning procedures. For equipment that should not be exposed to water, other validated cleaning and disinfection methods should be used.
Application method: Depending on equipment structure and hygienic design, wiping, spraying, circulation cleaning, or other validated methods may be selected. Adequate surface coverage should be achieved while avoiding liquid accumulation or disinfectant entering areas that are not designed for water exposure.
Contact time: Contact time should strictly follow the specific product instructions and the company’s validation results. Insufficient contact time may reduce disinfection performance, while unnecessarily prolonged exposure may increase material exposure and the burden of subsequent residue removal.
Temperature: The operating temperature should comply with the product instructions. Elevated temperatures may accelerate chlorine dioxide volatilization or reduce working-solution stability, thereby affecting the actual effective concentration.
If rinsing is required by the product instructions or by the company’s validated procedures, water meeting the applicable hygiene requirements for food production should be used to avoid introducing new contamination during rinsing.
If rinsing is required, it should be carried out according to the established procedure after the specified contact time has been completed, while avoiding abnormal drying of the disinfectant solution on the equipment surface.
For equipment areas designed for wet rinsing or CIP, flowing water may be used to rinse the required surfaces. For complex equipment, pipelines, valves, and hygienically difficult areas, the process should ensure sufficient exchange of the rinsing medium to remove residues effectively.
Rinsing time and water volume should be determined according to equipment design, flow rate, and residue-validation results. A universal rinsing time of 3–5 minutes should not be applied to all equipment.
For surfaces that directly contact the product, the absence of obvious odor may be used only as a supplementary sensory indication and should not replace quantitative or semi-quantitative residue testing.
If manual wiping is used, dedicated hygienic tools that meet the company’s sanitation-management requirements should be used. Procedures for replacement, cleaning, and storage should also be established to prevent cross-contamination.
Where appropriate and where the equipment design permits, dedicated cleaning systems such as CIP may be used. Programmed control of flow rate, time, and coverage can improve process reproducibility.
After rinsing or cleaning, abnormal odors may be checked under safe operating conditions to determine whether any obvious irritating or unusual odor remains.
Sensory inspection should only be used as a rapid supplementary screening method and should not be the sole basis for determining whether residues are acceptable.
According to the test method instructions, chlorine dioxide-compatible colorimetric methods, rapid test tools, or other field methods may be used to test the final rinse water or surface extracts collected according to a defined sampling procedure.
Results should be below the company’s predefined acceptable limit. Where appropriate, they may also be required to fall below the detection or quantification limit of the selected analytical method, depending on method performance and validation results.
Attention should also be paid to reagent expiration dates, applicable measurement ranges, and potential interference from other oxidants or the sample matrix.
The frequency of laboratory verification should be determined according to risk level, process stability, equipment changes, and historical data. Verification should be increased whenever the disinfection procedure changes or abnormal results are observed.
Quantitative analysis should use a validated method that is suitable for the target concentration range and provides sufficient sensitivity and selectivity. Potential interference from the sample matrix, such as rinse water or surface extracts, should also be evaluated.
Results should remain below the company’s predefined acceptable limits.
When the disinfection process is significantly changed or periodic verification is required, small-scale trial production may be conducted for chocolate or confectionery products.
Sensory evaluation: Trained evaluators can assess whether abnormal odors or flavor changes are present.
Crystal analysis: Where required by the process, methods such as Differential Scanning Calorimetry (DSC) may be used to support evaluation of chocolate crystal structure and thermal behavior. However, results should be interpreted together with tempering conditions, formulation, cooling, and storage conditions. Crystal changes should not automatically be attributed to chlorine dioxide residues.
Accelerated testing: According to the company’s product-stability validation program, bloom, flavor, and surface changes can be monitored during storage.
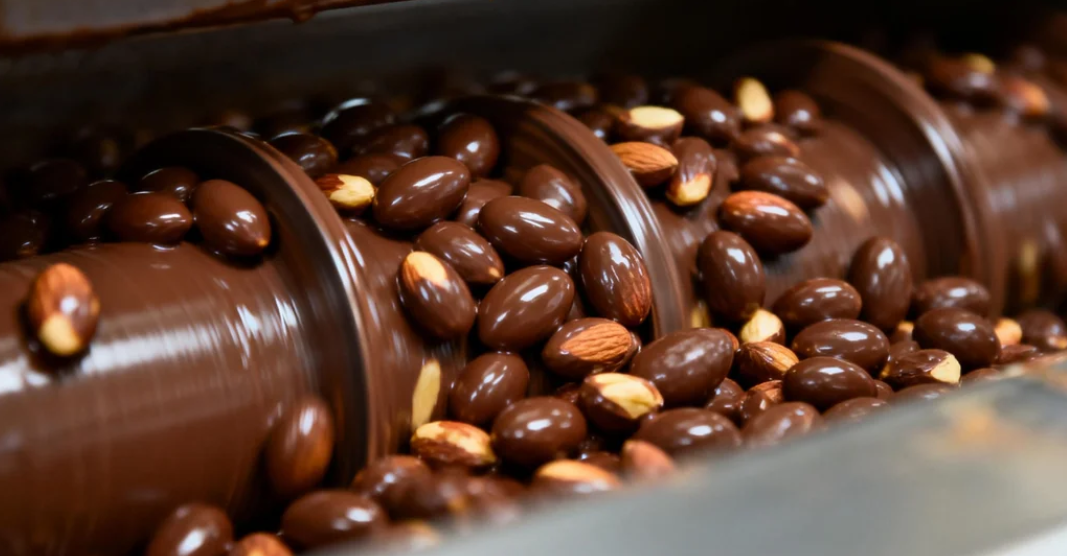
In the chocolate and confectionery industry, where flavor and texture are critical, disinfection and residue control are not simply routine cleaning steps. They require a careful balance between hygiene safety, product quality, and process stability.
Through source control, process optimization, rigorous verification, and systematic management, chlorine dioxide can complete its disinfection role while its residues are effectively controlled, minimizing unnecessary impact on subsequent production and product quality.
For low-moisture foods such as chocolate, professional cleaning and disinfection should not simply mean “using more rinse water until nothing remains.” Instead, whether rinsing is required, how it should be performed, and how residue acceptability should be verified must be determined according to equipment hygienic design, product instructions, and the company’s validated sanitation procedures.
This approach not only supports compliance with hygiene requirements, but also demonstrates a commitment to consumers and to consistent product quality.
The reddish color of fermented tofu cannot be determined solely by its appearance; sampling and testing are necessary, and the abnormal product must be isolated. Relying solely on disinfectants is insufficient; equipment and the workshop environment must be thoroughly investigated. Air disinfection requires unmanned operation and material isolation. Disinfectants should be used according to specifications, and problems should be identified through a combination of production records and testing.
AB cleaning agents in food factories are prone to producing odor residues; Chlorine dioxide disinfectant can sterilize and deodorize without harmful residues. It can be diluted and used for disinfection of workshop equipment and water bodies, with matching ratios and safety operation requirements.
Chlorine dioxide disinfection in food production will produce harmful residues, and the water consumption of traditional large water washing is serious. Four measures can be taken to save water and reduce waste on the basis of ensuring food safety, so as to help enterprises achieve multiple benefits and win-win results.
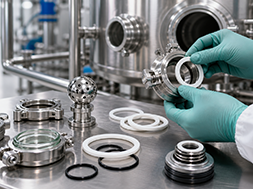
While switching from sodium hypochlorite to chlorine dioxide disinfection offers advantages such as sterilization, biofilm removal, and fewer disinfection byproducts, the strong oxidizing properties of chlorine dioxide necessitate careful consideration of production line material compatibility: 316L stainless steel should be prioritized for piping, and fluororubber or polytetrafluoroethylene (PTFE) should be used for seals, while also considering the suitability of accessories such as sight glasses and spray nozzles. The switch can be smoothly completed in three steps: establishing material records, conducting a 72-hour immersion test, and carrying out small-scale trial runs and inspections, thus preventing equipment corrosion and damage.
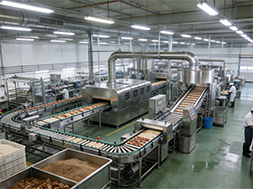
Traditional chlorine dioxide disinfection in food factories is time-consuming and reduces production capacity. Addressing pain points such as solution preparation, spraying, and ventilation monitoring, the process can be optimized in stages through equipment upgrades, zoned disinfection, scientific control of disinfection parameters, and accelerated ventilation monitoring. This phased process optimization, while ensuring safety and compliance, can shorten disinfection time by 30-50%, freeing up production capacity and improving hygiene management.
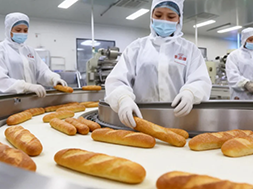
Powdered milk powder and starch dust in the powdered food workshop will absorb and consume chlorine dioxide dry fog, reducing the disinfection effect. It can solve the disinfection problems caused by dust and ensure food safety by reducing dust before disinfection, regulating the particle size of dry fog, pulse releasing agent, optimizing the air flow in the workshop, and matching other disinfection methods.
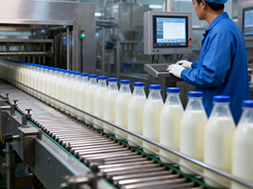
Chlorine dioxide is widely used for disinfection in water supply and food supply chains, but current issues exist regarding standards, procedures, and residue monitoring. It is necessary to standardize operating procedures, establish a comprehensive residue monitoring system, and improve risk warning and emergency response mechanisms to ensure disinfection safety from water treatment plant to table.
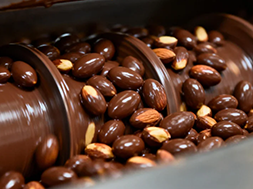
When using chlorine dioxide for disinfection of chocolate equipment, it is necessary to control the residue of the agent to avoid damaging the flavor and quality of the product. The preparation of the agent should be standardized, the disinfection and rinsing process optimized, and residue compliance verified through multiple methods. Since chocolate is a low-moisture food, a customized cleaning plan needs to be developed based on the specific equipment to balance safety and production stability.
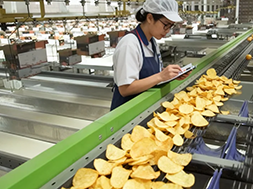
The strong oxidizing properties of chlorine dioxide can cause plastic conveyor belts in food factories to oxidize and age, with different materials exhibiting varying degrees of tolerance. To address this, a more refined approach can be taken, including controlling the concentration, shortening contact time, selecting oxidation-resistant materials, and employing differentiated disinfection methods and rotating disinfectants, thus balancing disinfection effectiveness with equipment protection.
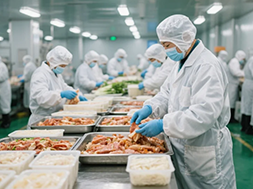
When using chlorine dioxide for disinfection in food production, the disinfectant concentration is a critical control point in the HACCP system. Test strips are convenient to use but have a relatively large margin of error; portable testing instruments offer higher accuracy but require regular calibration and maintenance. Enterprises can adopt a three-tiered monitoring solution: primarily online sensors, supplemented by portable instrument inspection and calibration, and emergency verification using test strips. This enables continuous monitoring, data retention and traceability, ensuring both disinfection effectiveness and food safety.
Northeast of Huangshan Road and Chuangye Intersection, Small and Medium sized Enterprise Entrepreneurship Industrial Park, Shanwang Town, Linqu County, Weifang City, Shandong Province
Copyright © 2025 by Shandong Huashi Pharmaceutical Co., Ltd All Rights Reserved


 Language
 中文
 Русский
 Chlorine Dioxide Disinfectant Manufacturer


