Welcome to Our Factory for a Visit! Free customized disinfection solutions
Switching a disinfection system from sodium hypochlorite, which may have been used for decades, to chlorine dioxide may appear to be a simple change. In reality, it can involve a systematic transformation covering equipment, technical knowledge, and management.
For the drinking water industry, this is not merely a change in disinfection technology. It may also bring changes to equipment, monitoring, staff training, and operational management.
Traditional sodium hypochlorite systems are mature and relatively easy to operate, but under conditions such as high organic loads, control of specific pathogens, and management of disinfection by-products, they may face certain challenges.
Under some water-quality conditions, chlorine dioxide can provide effective microbial control, is relatively insensitive to changes in pH, and may reduce the formation of certain by-products associated with conventional chlorination. At the same time, however, attention must be paid to chlorite, chlorate, on-site generation, and operational control.
It should be emphasized that chlorine dioxide treatment is not free of by-products. Operational management should specifically address the formation and control of chlorite and chlorate.
During the initial transition period, water plants often face the challenge that “equipment may be easier to replace than established operating habits.”
The experience that long-term employees have gained from operating sodium hypochlorite systems may become an obstacle when learning a new system. Chlorine dioxide systems differ significantly from sodium hypochlorite systems in terms of generation, dosing control, safety management, and water-quality monitoring. Operators therefore need to move from “memorized operation” to “understanding-based operation.”
Compared with direct sodium hypochlorite dosing, chlorine dioxide systems often involve on-site generation, raw-material proportioning, generation efficiency, gas-liquid safety, and online interlock controls, placing higher requirements on equipment management and operating discipline.
The introduction of a chlorine dioxide system requires operating personnel to understand the water chemistry associated with chlorine dioxide generation, dosing, monitoring, and by-product control.
They need to understand how chlorine dioxide behaves under different water-quality conditions, learn to interpret more complex monitoring data, and even anticipate chemical changes that may occur during the disinfection process.
After switching systems, one water plant conducted a three-month technical training program covering equipment operation, redox principles, and other relevant topics.
Following systematic training, operators are generally better able to manage equipment operation, dosing control, and abnormal operating conditions, thereby improving system stability and response capability.
At first glance, the initial investment in a chlorine dioxide system may be higher than that of a sodium hypochlorite system. However, a life-cycle cost analysis may present a different picture.
Changes in chemical costs: Chlorine dioxide has strong oxidizing capacity and, under certain water-quality conditions and for certain target microorganisms, may achieve the desired disinfection effect at relatively low dosing levels.
In some projects, if chlorine dioxide can reduce the actual required dose or lower the burden on other treatment stages, the overall chemical cost may be optimized. However, whether it is actually lower than sodium hypochlorite must be evaluated based on local chemical prices and actual operating conditions.
Impact on distribution-system maintenance: Chlorine dioxide can be used for microbial control and can oxidize certain forms of dissolved iron and manganese. However, the resulting oxidized particles still need to be removed through downstream treatment or distribution-system management. Its actual impact on flushing frequency and maintenance costs therefore depends on the specific water quality and system conditions.
Changes in safety-management costs: Sodium hypochlorite storage requires attention to leakage prevention, corrosion resistance, storage space, and other safety-management requirements.
Chlorine dioxide is generally generated on site and used on demand, which can reduce the need to store highly concentrated chlorine dioxide as a finished product. However, it also introduces additional safety requirements relating to precursor storage, generator operation, ventilation, leak detection, and interlock control.
Once the disinfection system has been switched and the team’s technical knowledge has been updated, the overall operation of the water plant may undergo significant changes.
Redesign of management processes: Processes ranging from procurement and storage to dosing and monitoring may need to be redesigned. Many water plants use such transitions as an opportunity to introduce intelligent control systems, enabling automatic adjustment and remote monitoring of the disinfection process.
Stronger cross-department collaboration: Chlorine dioxide system operation often requires close coordination among process, equipment, laboratory, and safety teams. Establishing such cross-functional cooperation can help improve overall plant operating efficiency.
Improved emergency response: If emergency procedures, interlock protection, and personnel training are established specifically for the chlorine dioxide system, the plant can improve its ability to respond to equipment failures and fluctuations in water quality. The experience gained from this emergency-management approach may also provide useful lessons for other process areas.
Improved water-quality management: Under suitable water-quality conditions, chlorine dioxide can help reduce the formation of certain conventional chlorination by-products. However, chlorite, chlorate, and other relevant indicators must still be controlled. Ultimately, performance should be evaluated according to actual analytical results for finished water and distribution-system water.
Despite its potential advantages, many water plants still treat the transition to chlorine dioxide primarily as an “equipment replacement” project and fail to fully realize its broader system value.
Common shortcomings include:
Insufficient training: There is often more emphasis on operational procedures than on underlying principles, limiting the team’s ability to deal with non-standard or abnormal conditions.
Underutilization of data: If data such as flow rate, chemical dosage, generator operating status, residual levels, and related water-quality monitoring results are used only for routine alarms and recordkeeping, their potential value for process optimization cannot be fully realized.
Outdated management practices: Some plants may continue to use management methods and performance indicators developed for their previous sodium hypochlorite systems.
A true system transition requires management to treat the project as an integrated initiative involving technology, people, and the management system.
This may involve adjusting organizational structures, updating performance indicators, rebuilding knowledge-management systems, and even modifying decision-making processes.
The transition from sodium hypochlorite to chlorine dioxide may appear to be a change in disinfection technology. However, if the transition also drives improvements in automation, data management, personnel training, and operating standardization, it can help the water plant move toward a more data-driven and standardized operating model.
The real value of such a system adjustment is reflected not only in changes in water-quality control and operating costs, but also in stronger professional capabilities among staff and the modernization and standardization of the operating system.
As night falls and the water plant remains brightly lit, the new system runs steadily while operators calmly analyze the changing data on their screens. At that moment, what we see is not merely the upgrading of a single water plant, but a solid step by the industry toward safer, more efficient, and more sustainable drinking water supply.
Chlorine dioxide can efficiently disinfect drinking water, is not easy to generate carcinogenic disinfection by-products, and will produce chlorite and other residues, which must comply with the national standard limits. It shall be accurately added according to the water quality and equipped with qualified equipment and process. The safety of compliant use is high. Water supply enterprises need to do a good job in control and monitoring to ensure the safety of water quality.
Chlorine dioxide is a who Certified grade A1 safe disinfectant with high sterilization efficiency, few harmful by-products, strong water quality adaptability and multiple water purification functions; Compared with traditional chlorine disinfection, it is safer and more environmental friendly, and can be widely used in drinking water, sewage treatment, food and beverage disinfection and other fields.
Chlorine dioxide can sterilize and remove odors in water treatment plants and is unlikely to generate trihalomethanes. However, in practical applications, it can fail to remove odors or even produce new unpleasant smells. Organic matter in the water source, bromide ions, and low temperatures can affect treatment effectiveness. Furthermore, its removal capacity for geosmin and 2-methylisoborneol is limited, and improper dosage can also cause odor problems. Water treatment plants need to strengthen water quality monitoring, dynamically adjust dosages, and, when necessary, combine ozone-activated carbon processes to ensure that the odor of the treated drinking water meets standards.
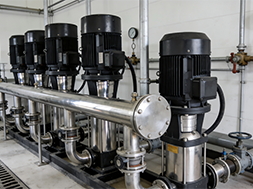
When adding chlorine dioxide to the water pumping station to maintain residual chlorine in the pipeline network, it is necessary to avoid pipeline corrosion caused by local high concentrations. The dosage should be accurately controlled by flow-linked dosing, pipeline mixing, and online residual chlorine monitoring, while also paying attention to under-scale corrosion, thus balancing disinfection and pipeline protection.
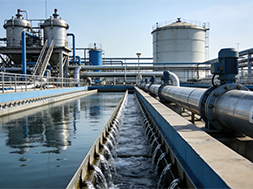
Pipeline network renovations can easily alter the hydraulic conditions of the network, increasing flow velocity and creating stagnant zones that consume chlorine dioxide, leading to fluctuations in water quality. Water plants can ensure the quality of water supplied to the end points through monitoring and prediction, dynamic chemical dosing, pipeline flushing, and the activation of contingency plans.
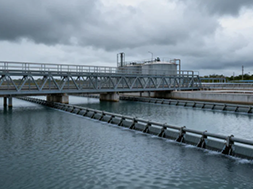
Traditional chlorine disinfection is prone to producing carcinogenic halogenated by-products; chlorine dioxide oxidizes and kills bacteria, with almost no such by-products, good inactivation effect, and the ability to remove odor and inhibit algae, but it generates by-products such as chlorite, requires higher raw material and operation and maintenance costs, and is suitable for water plants that can be upgraded and managed in a coordinated manner, rather than being simply and directly replaced.
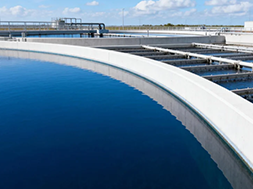
This study simulates a scenario where a small town's water plant experiences a sudden pollution outbreak caused by medical wastewater and the failure of chlorine dioxide disinfection. It analyzes the reasons why pollutants consume disinfectant and provides four-step emergency response measures. Furthermore, it proposes long-term improvement suggestions in terms of monitoring, supplies, contingency plans, and drills to enhance the emergency response capabilities of small and medium-sized water plants.
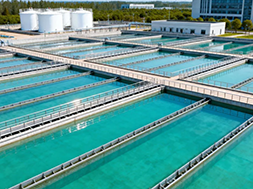
Switching from sodium hypochlorite to chlorine dioxide disinfection in water plants is not just about replacing equipment; it's a complete system upgrade. Chlorine dioxide disinfection is more effective, produces fewer byproducts, and has lower overall costs. However, many water plants only replace the hardware, neglecting personnel training and adapting management systems. The core of this transformation is shifting from experience-based to scientific operation.
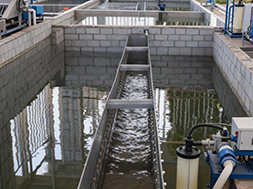
The actual dosage of chlorine dioxide at water treatment plants often exceeds the theoretical value, influenced by factors such as reducing agents in the water, sediment in the pipe network, water quality fluctuations, and byproduct consumption. By leveraging monitoring and local operational data to optimize dosage, we can provide water quality assessments and customized dosage solutions.
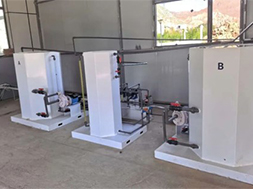
A water plant in a county in Qinghai Province with a capacity of 30,000 cubic meters per day was found to have excessive byproducts from sodium hypochlorite disinfection. It was upgraded to a Xiuba chlorine dioxide dosing system. Four on-site tests showed that residual chlorine dioxide in the effluent was within acceptable limits, achieving stable compliance. Water treatment upgrades need to be tailored to specific on-site conditions to create a complete closed-loop disinfection process.
Northeast of Huangshan Road and Chuangye Intersection, Small and Medium sized Enterprise Entrepreneurship Industrial Park, Shanwang Town, Linqu County, Weifang City, Shandong Province
Copyright © 2025 by Shandong Huashi Pharmaceutical Co., Ltd All Rights Reserved


 Language
 中文
 Русский
 Chlorine Dioxide Disinfectant Manufacturer


